What is GHP Certification? Good Hygiene Practices & Contamination Prevention
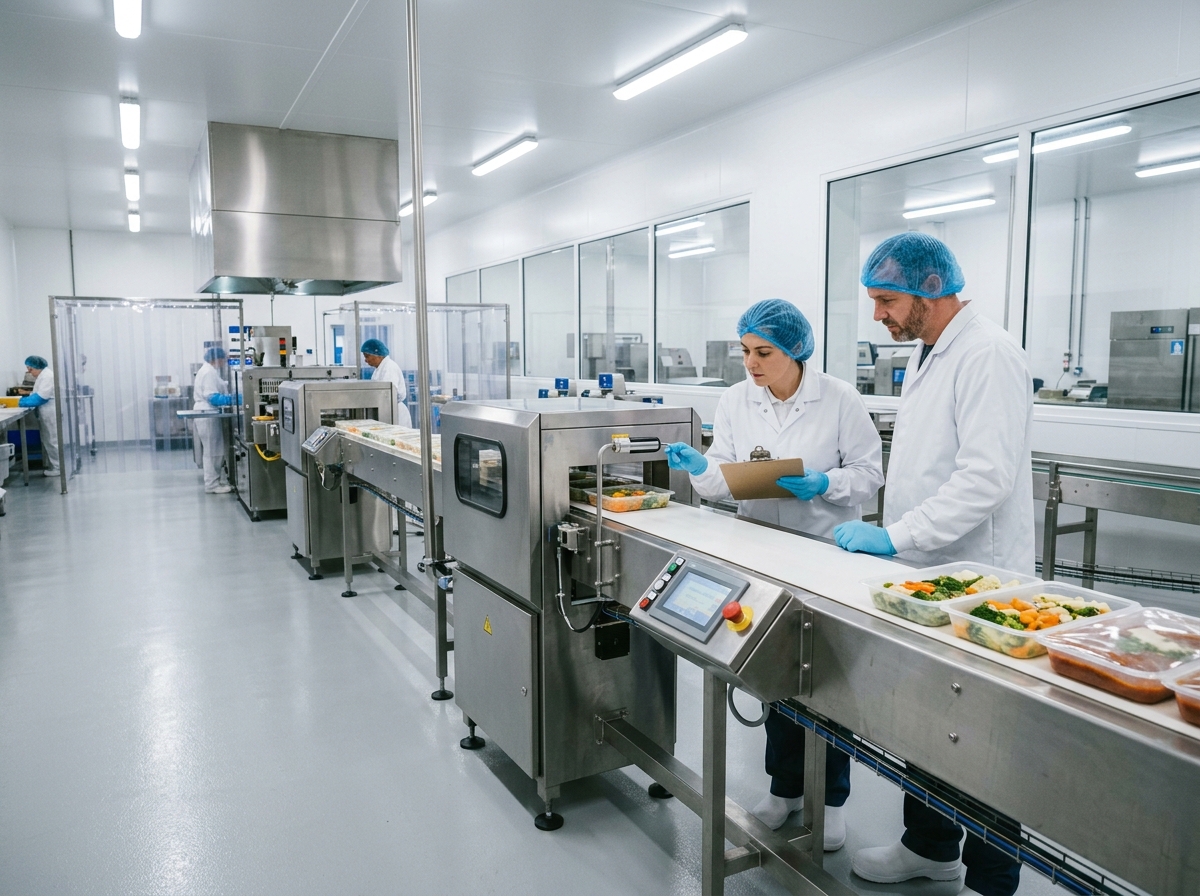
GHP (Good Hygiene Practices) Certification verifies that organizations involved in food production, processing, handling, and distribution maintain high standards of hygiene and sanitation. GHP is a foundational element of food safety systems, ensuring that food products are safe, clean, and fit for consumption by minimizing contamination risks throughout the supply chain.
Pristine Sanitation & Prerequisite Foundation for HACCP
Good Hygiene Practices serve as the mandatory foundation for advanced food safety programs, ensuring clean facilities, personnel sanitation protocols, and pest-free environments that protect consumers from foodborne hazards.
GHP Certified
Good Hygiene Practices CompliantKey Objectives of GHP Certification
Essential sanitation benchmarks designed to safeguard product cleanliness and build consumer trust:
Promote Proper Hygiene and Sanitation
Establish and maintain effective cleaning, personal hygiene, and facility sanitation practices.
Prevent Food Contamination
Reduce risks of physical, chemical, and biological hazards in food products.
Support Compliance with Food Safety Regulations
Align operations with national and international hygiene standards.
Build Consumer Confidence
Demonstrate commitment to safe and hygienic food handling.
Scope of GHP Certification
GHP encompasses comprehensive hygiene protocols across all operational stages:
Facility Cleanliness & Sanitation
Facility cleanliness and sanitation.
Personnel Hygiene & Training
Personnel hygiene and training.
Equipment Maintenance & Cleaning
Equipment maintenance and cleaning.
Pest Control & Waste Management
Pest control and waste management.
Safe Food Handling & Storage Practices
Safe food handling and storage practices.
Benefits of GHP Certification
Direct commercial, regulatory, and public health benefits for food businesses:
Enhanced Food Safety and Quality
Ensures production environments are clean and hygienic.
Regulatory Compliance
Meets requirements of food safety authorities and supports HACCP implementation.
Reduced Risk of Foodborne Illnesses
Minimizes contamination and spoilage risks.
Improved Operational Efficiency
Streamlines hygiene processes and staff training.
Stronger Market Reputation
Boosts consumer and stakeholder trust in your brand.
Who Should Obtain GHP Certification?
Foundational hygiene compliance for organizations across the food supply chain:
Food Manufacturers & Processors
Food manufacturers and processors.
Catering & Hospitality Services
Catering and hospitality services.
Storage & Distribution Centers
Food storage and distribution centers.
Retail Outlets & Supermarkets
Retail food outlets and supermarkets.
Food Supply Chain Organizations
Any organization involved in the food supply chain.
Strengthen Food Safety with GHP Certification
Achieving GHP Certification is a critical step toward ensuring hygienic food production and handling practices, enhancing food safety, and building trust with consumers and regulatory bodies.
